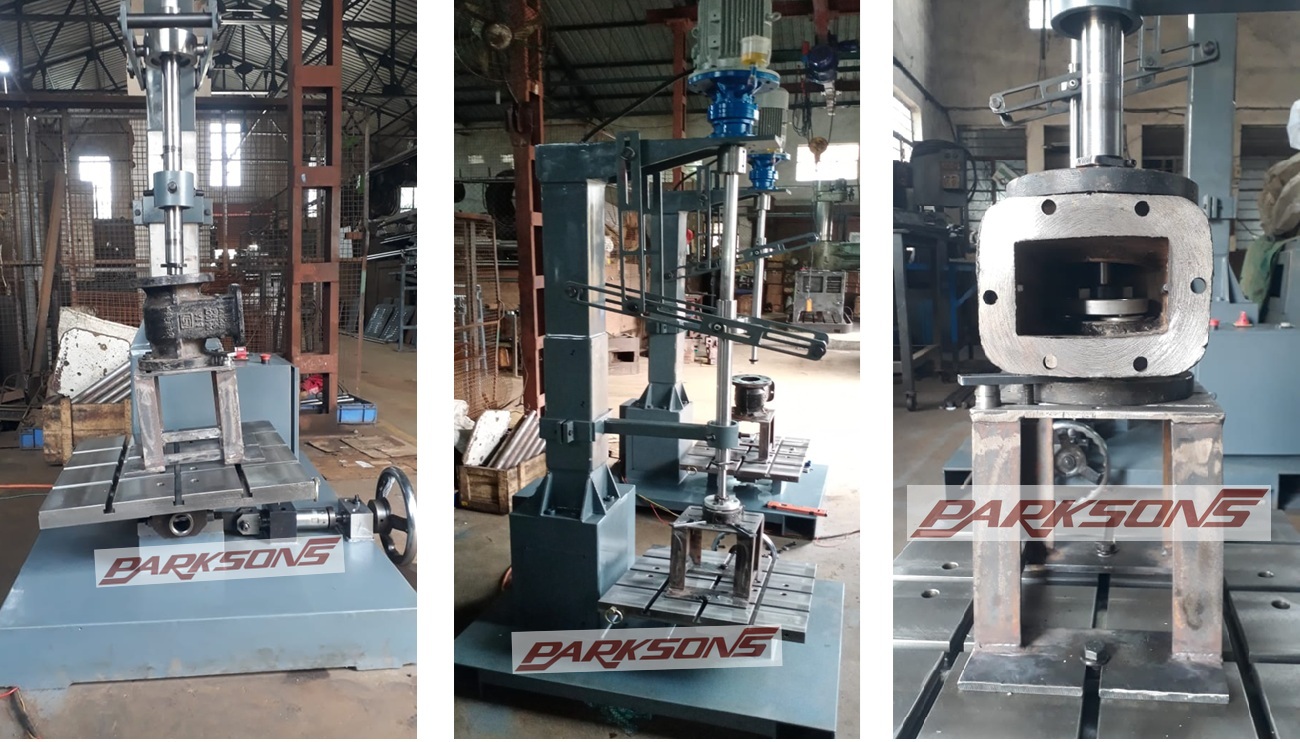
Stationary Valve Grinding & Lapping Machine
BHEL Maitree Super Thermal Power Project, 2 × 660 MW, Bangladesh
A workshop-based solution for controlled reconditioning of valve sealing faces and flanges, replacing inconsistent manual lapping practices during shutdown maintenance.
Why Standard Methods Fall Short
Portable lapping tools and manual grinding arrangements are adequate for small or infrequent jobs. However, they struggle to deliver repeatable results when valve sizes vary widely, angular alignment must be maintained, and work is constrained by tight outage windows. Without a rigid reference, even experienced technicians produce variable outcomes leading to rework.
How the Solution Was Framed
- Rigid work holding to establish a consistent reference plane.
- Adjustable angular alignment to handle different valve geometries.
- Controlled low-speed rotation suitable for fine lapping.
Key Technical Parameters
If valve reconditioning is a recurring activity during shutdowns, variability in sealing quality often originates from the maintenance method rather than the valve itself.
Evaluate if this approach fits your workshop